1. Toyota Material Handling
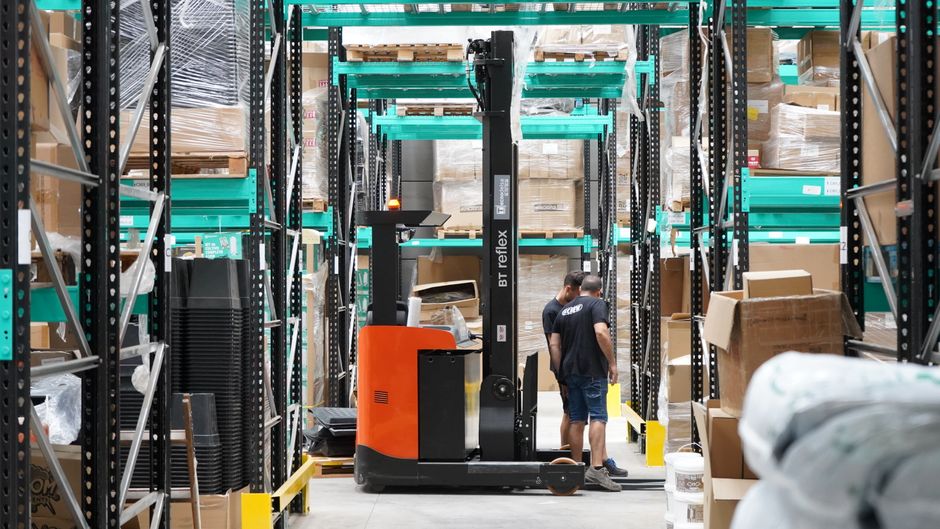
Toyota Material Handling is the world's largest manufacturer of forklifts and a dominant force in the material handling equipment industry. Formed through the integration of Toyota's forklift division with BT Industries and Raymond Corporation, the company offers a comprehensive portfolio that includes counterbalanced forklifts, reach trucks, order pickers, tow tractors, and automated guided vehicles (AGVs). Its global network spans more than 200 countries, supported by thousands of dealership locations and service centers.
The company is widely recognized for its Toyota Production System, which ensures consistent quality, durability, and low total cost of ownership. Toyota's electric forklifts and lithium-ion battery solutions have gained significant traction as warehouses shift toward greener operations. Additionally, its advanced telematics platform, Toyota I_Site, helps fleet managers monitor usage, optimize maintenance, and reduce energy costs.
For businesses seeking reliable equipment backed by extensive aftermarket support, Toyota Material Handling remains a top choice. Its commitment to safety, innovation, and sustainability keeps it at the forefront of the global market.
2. KION Group (Linde Material Handling & STILL)
Germany-based KION Group is a global leader in intralogistics, operating through well-known brands such as Linde Material Handling, STILL, and Dematic. Linde focuses on premium counterbalanced trucks and warehouse equipment, while STILL specializes in customized intralogistics solutions. Together, they cover nearly every material handling need, from pallet trucks to complex automated warehouse systems.
KION's strength lies in its engineering excellence and its ability to integrate hardware with software. The group's Dematic division provides conveyor systems, sortation equipment, and warehouse execution software, making KION a one-stop shop for automated supply chain solutions. Its fuel-cell and lithium-ion powered trucks also support emission-free operations.
With a presence in over 100 countries and a strong focus on Industry 4.0, KION Group continues to shape the future of intralogistics. Companies looking for high-performance equipment and smart automation will find KION's brands highly competitive.
3. Jungheinrich
Jungheinrich is a German intralogistics specialist known for its innovative warehouse equipment and automation solutions. The company manufactures forklifts, reach trucks, stackers, order pickers, and pallet trucks, along with racking systems and warehouse management software. Its product range is designed to improve efficiency in narrow aisles and high-density storage environments.
Jungheinrich has been a pioneer in lithium-ion technology, offering a wide range of trucks with maintenance-free batteries. The company's automated guided vehicles and mobile robots help warehouses address labor shortages and increase throughput. Its Jungheinrich Warehouse Management System (WMS) provides real-time visibility and control over inventory and material flow.
With a strong European base and expanding global reach, Jungheinrich is a preferred partner for businesses seeking energy-efficient and automated material handling solutions. Its emphasis on research and development ensures a steady stream of cutting-edge products.
4. Crown Equipment Corporation
Crown Equipment Corporation is a privately held American manufacturer with a reputation for durable, operator-focused forklifts and warehouse equipment. The company produces electric counterbalanced forklifts, reach trucks, order pickers, pallet trucks, and turret trucks, many of which are designed for demanding applications in food and beverage, retail, and manufacturing.
Crown's vertical integration allows it to control quality at every stage, from component manufacturing to final assembly. Its innovative designs, such as the Crown Wave Work Assist Vehicle and the QuickPick Remote order picking system, enhance productivity and safety. The company also offers fleet management tools and comprehensive service programs.
Known for its strong dealer network and customer-centric approach, Crown is a trusted name in North America and beyond. Businesses that prioritize ergonomics and reliability often turn to Crown for their material handling needs.
5. Hyster-Yale Materials Handling
Hyster-Yale Materials Handling is a global designer, engineer, and manufacturer of lift trucks and aftermarket parts. Its brands, Hyster and Yale, offer a broad range of forklifts, including internal combustion, electric, and specialized models for ports, containers, and rough terrain. The company also provides automated guided vehicles and telemetry solutions.
Hyster-Yale focuses on application-specific solutions, helping customers optimize their fleets for specific industries such as logistics, construction, and manufacturing. Its hydrogen fuel cell and lithium-ion options support sustainability goals. The company's global dealer network ensures responsive service and parts availability.
With a history dating back to the early 20th century, Hyster-Yale combines deep industry knowledge with modern innovation. It remains a top choice for heavy-duty and high-performance material handling equipment.
6. Mitsubishi Logisnext
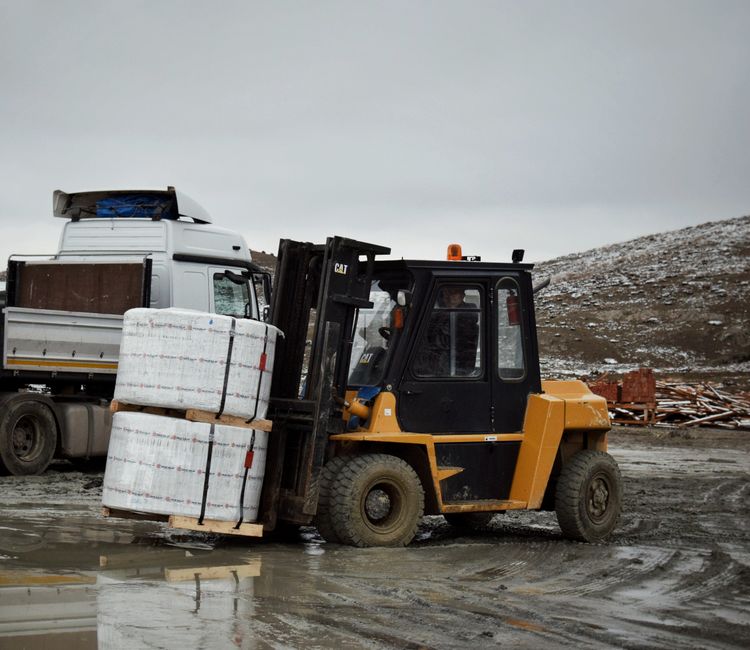
Mitsubishi Logisnext is a Japanese multinational formed by the integration of Mitsubishi Nichiyu Forklift, UniCarriers, and other brands. It offers a wide range of forklifts, warehouse equipment, and automated solutions under brands like Mitsubishi, Cat Lift Trucks, UniCarriers, and TCM. The company serves diverse markets, from small warehouses to large ports.
Logisnext emphasizes energy efficiency and environmental performance, with electric and hybrid models that reduce emissions. Its automated guided vehicles and fleet management systems help businesses streamline operations. The company's global manufacturing and distribution network ensures local support.
Through continuous innovation and strategic partnerships, Mitsubishi Logisnext has established itself as a major player in the global material handling industry. Its diverse brand portfolio caters to a wide spectrum of customer needs.
7. Doosan Industrial Vehicle
Doosan Industrial Vehicle, part of the Doosan Group, is a leading manufacturer of forklifts, reach trucks, and warehouse equipment. The company is known for its robust diesel, LPG, and electric forklifts, which are used in construction, manufacturing, and logistics. Its products are designed for high performance and durability in tough environments.
Doosan has expanded its electric lineup with lithium-ion battery options and advanced ergonomic features. The company also offers telematics and fleet management solutions to improve operational efficiency. Its global dealer network provides sales, service, and parts support.
With a focus on quality and customer satisfaction, Doosan Industrial Vehicle continues to grow its presence in both mature and emerging markets. It is a reliable choice for businesses seeking cost-effective and dependable equipment.
8. Clark Material Handling Company
Clark Material Handling Company is an American manufacturer with a long history in the forklift industry, dating back to 1917. The company produces a full line of internal combustion and electric forklifts, pallet trucks, stackers, and tow tractors. Clark is known for its durable and easy-to-maintain equipment.
Clark's forklifts are engineered for performance and operator comfort, with features like ergonomic controls and advanced cooling systems. The company offers a range of power options, including diesel, LPG, and electric, to suit different applications. Its dealer network provides comprehensive support across North America and other regions.
Clark remains a trusted brand for businesses that value reliability and simplicity. Its commitment to quality and service has kept it relevant in a highly competitive market.
9. Combilift
Combilift is an Irish manufacturer specializing in multidirectional forklifts, side loaders, and articulated forklifts. Its innovative designs allow for safe and efficient handling of long loads, such as timber, steel, and pipes, in narrow aisles. Combilift's products are known for their space-saving capabilities and versatility.
The company's range includes the Combi-CB, Combi-RT, and Combi-SC models, which can operate in tight spaces and reduce the need for multiple machines. Combilift also offers custom solutions tailored to specific industry needs. Its global distribution network supports customers in over 85 countries.
With a focus on innovation and customer collaboration, Combilift has won numerous awards for its engineering. It is a top choice for businesses looking to optimize storage density and handling efficiency.
10. Anhui Heli Co., Ltd.
Anhui Heli Co., Ltd. is one of China's largest forklift manufacturers and a major player in the global material handling market. The company produces a wide range of forklifts, including electric, internal combustion, and warehouse equipment, under the Heli brand. Its products are exported to over 150 countries.
Heli invests heavily in research and development, with a focus on electric and intelligent forklifts. The company offers lithium-ion battery options and automated guided vehicles. Its large-scale manufacturing capabilities allow for competitive pricing without compromising quality.
As global demand for material handling equipment grows, Anhui Heli continues to expand its international footprint. It is a strong contender for businesses seeking cost-effective and reliable solutions.
Conclusion
Choosing the right material handling equipment manufacturer depends on your specific needs, budget, and operational requirements. The top 10 manufacturers listed above represent the best in the industry, offering a mix of innovation, reliability, and global support. Whether you need a simple pallet truck or a fully automated warehouse system, these companies have the expertise and product range to deliver.
When evaluating manufacturers, consider factors such as total cost of ownership, aftermarket support, energy efficiency, and compatibility with your existing systems. By partnering with a reputable manufacturer, you can improve productivity, safety, and profitability in your material handling operations.