 English
 简体中文
 Русский
 Español
 Deutsch
Supply programme
Top 10 Chemical Raw Material Suppliers in China
Discover the top 10 chemical raw material suppliers in China, from Sinopec to Wanhua. Compare products, strengths, and sourcing tips. Start your search today!
Why China Dominates the Chemical Raw Materials Market
China is the world's largest producer and exporter of chemical raw materials, supplying everything from basic petrochemicals and inorganic acids to fine chemicals, pharmaceutical intermediates, and specialty additives. With an extensive industrial base, integrated supply chains, and competitive pricing, Chinese suppliers serve buyers across North America, Europe, Southeast Asia, and the Middle East. For manufacturers, formulators, and trading companies, choosing the right partner in China is critical to product quality, regulatory compliance, and supply stability.
In this guide, we profile ten of the most influential chemical raw material suppliers in China, based on scale, product range, export experience, and industry reputation. Whether you need bulk commodity chemicals or niche specialty ingredients, these companies are a strong starting point for your sourcing strategy.

1. Sinopec (China Petroleum & Chemical Corporation)
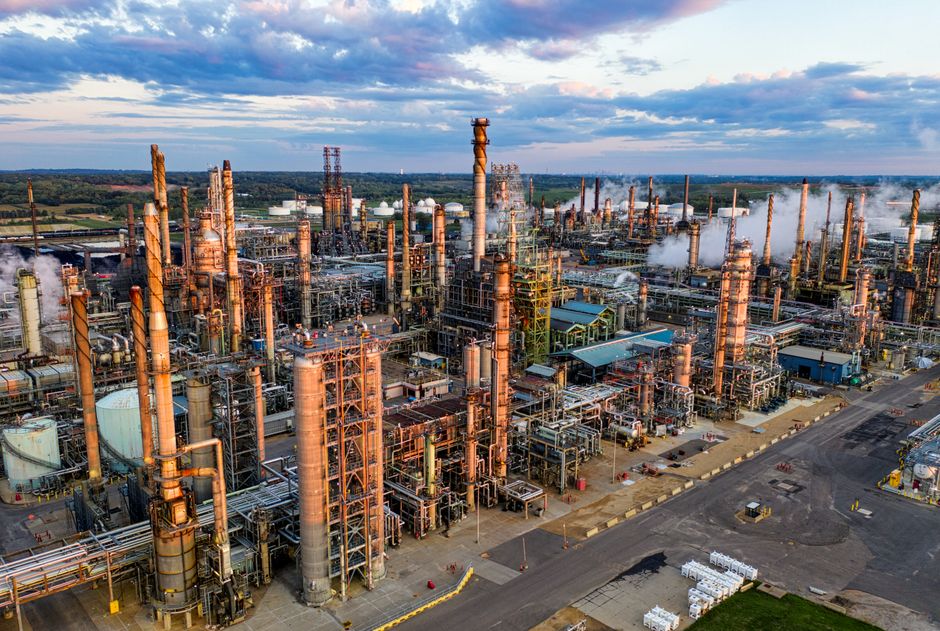
Sinopec is one of the largest integrated energy and chemical companies in the world and a cornerstone of China's chemical raw materials industry. Its chemical segment produces ethylene, propylene, benzene, toluene, xylene, synthetic resins, synthetic rubber, and a wide range of petrochemical intermediates used in plastics, textiles, coatings, and packaging.
Because Sinopec controls refining and cracker capacity at massive scale, it offers reliable supply volumes and consistent specifications, which is essential for large industrial buyers. The company also invests heavily in R&D, so its portfolio continues to expand into higher-value specialty chemicals and new materials.
Key strengths
- Enormous production capacity and nationwide logistics network
- Broad portfolio of commodity and intermediate chemicals
- Strict quality control and international certifications
2. PetroChina (China National Petroleum Corporation)
PetroChina is the listed arm of CNPC and another giant in China's petrochemical sector. It supplies olefins, aromatics, fertilizers, synthetic resins, and industrial solvents, with major production bases in Northeast and Northwest China.
For buyers of commodity raw materials such as urea, methanol, and polyethylene, PetroChina is often a primary source. Its integration with upstream oil and gas gives it cost advantages that translate into competitive export pricing.
PetroChina also works with international partners on technology licensing and joint ventures, which helps maintain global standards in product quality and environmental performance.
3. Wanhua Chemical Group
Wanhua Chemical is a world-leading producer of polyurethane raw materials, including MDI, TDI, and polyether polyols. It has grown from a regional player into a global competitor with production sites in China, Europe, and the United States.
The company is known for its proprietary technologies and vertical integration, which allow it to control costs and quality from basic feedstocks to finished polyurethane systems. Wanhua serves industries such as furniture, construction, automotive, and footwear.
Why buyers choose Wanhua
- Global-scale MDI and TDI capacity
- Strong technical support and application development
- Commitment to sustainability and low-carbon production
4. Rongsheng Petrochemical
Rongsheng Petrochemical operates one of the largest refining and chemical complexes in China, located in Zhejiang Province. Its integrated facility produces paraxylene (PX), purified terephthalic acid (PTA), ethylene, and polyester raw materials.
Rongsheng's scale allows it to serve high-volume customers in the polyester, textile, and packaging industries with consistent quality. The company has also formed strategic partnerships with international energy firms to secure feedstock and expand its global reach.
For buyers seeking PTA, PX, or polyester intermediates, Rongsheng is a supplier worth evaluating for long-term contracts.
5. Hengli Petrochemical
Hengli Petrochemical is another integrated refining and chemical giant, with major operations in Liaoning and Jiangsu. It produces PTA, ethylene glycol, polyester, and various petrochemical raw materials.
Hengli is recognized for its advanced manufacturing technology and efficient logistics, including dedicated port facilities that speed up export shipments. Its vertical integration from crude oil to polyester helps stabilize costs and supply.
The company's focus on digitalization and smart manufacturing also supports consistent product quality, a key factor for international customers.
6. Zhejiang Longsheng Group
Zhejiang Longsheng Group is a leading supplier of dyes, pigments, and textile chemicals. It serves the textile, leather, paper, and coatings industries with a broad range of intermediates and finished colorants.
Longsheng is known for its strong R&D capabilities and environmental management systems, which are increasingly important as global buyers demand compliance with REACH and other regulations.
Product highlights
- Disperse dyes and reactive dyes
- Organic pigments and intermediates
- Textile auxiliaries and specialty chemicals
7. Hubei Xingfa Chemicals Group
Hubei Xingfa Chemicals Group is one of China's largest producers of phosphorus-based chemicals, including yellow phosphorus, phosphoric acid, and phosphate salts. It also produces glyphosate and other agrochemical intermediates.
With integrated phosphorus mining and processing, Xingfa controls costs and ensures reliable supply. Its products are used in food, fertilizer, flame retardants, and water treatment applications.
For buyers of phosphorus derivatives, Xingfa is a strategically important supplier with significant export experience.
8. Jiangsu Yoke Technology
Jiangsu Yoke Technology specializes in organophosphorus flame retardants and specialty chemicals. It has become a key supplier to the electronics, construction, and automotive industries, where flame retardancy and thermal stability are critical.
The company invests in research and development to meet evolving safety and environmental standards, and it exports to markets in Europe, North America, and Asia.
Core products
- Organophosphorus flame retardants
- Polyurethane catalysts and additives
- Specialty fine chemicals
9. Zhejiang Juhua
Zhejiang Juhua is a major producer of fluorochemicals, including refrigerants, fluoropolymers, and inorganic fluorides. It is part of the Sinochem group and serves refrigeration, electronics, and new energy sectors.
As the world transitions to low-GWP refrigerants, Juhua has expanded its portfolio of environmentally friendly products, positioning itself as a forward-looking supplier.
Its fluorochemical raw materials are used in lithium batteries, semiconductors, and specialty coatings, making it a versatile partner for advanced industries.
10. Kingboard Chemical Holdings
Kingboard Chemical Holdings is a leading manufacturer of laminates, printed circuit board materials, and chemical raw materials such as methanol, phenol, acetone, and bisphenol A. It serves the electronics, automotive, and construction markets.
With integrated production and a global sales network, Kingboard offers reliable supply and technical support for customers in high-tech sectors.
Why it stands out
- Strong position in electronic-grade chemicals
- Integrated upstream and downstream operations
- Global distribution and customer service
How to Choose the Right Supplier
When evaluating chemical raw material suppliers in China, consider production capacity, quality certifications (ISO, REACH, FDA), export experience, and logistics capabilities. Request samples, audit facilities when possible, and clarify Incoterms, payment terms, and after-sales support. Building a long-term relationship with a reliable supplier can reduce risk and improve your competitiveness.
These ten companies represent different segments of China's chemical industry, from petrochemical giants to specialty chemical specialists. Depending on your product needs, one or more of them could become a key partner in your supply chain.
In scope
Browse all Materials frequently supplied with this programme
Keep reading
Other supply programmes
Chemical Raw Material Price Trends 2024: Full Outlook
Explore 2024 chemical raw material price trends, category forecasts, regional variations, and practical procurement tips to protect your margins. Read now.
View solutionTop 10 Chemical Raw Material Suppliers in China
Discover the top 10 chemical raw material suppliers in China, from Sinopec to Wanhua. Compare products, strengths, and sourcing tips. Start your search today!
View solutionHow to Verify Chemical Raw Material Quality: 7 Steps
Learn how to verify chemical raw material quality in 7 practical steps. From supplier audits to analytical testing—ensure safety and compliance. Read now!
View solutionHow to Choose a Reliable Chemical Raw Material Supplier
Learn how to choose a reliable chemical raw material supplier with our in-depth guide covering certifications, quality checks, pricing, and risk management.
View solutionStart a programme like this
Send the market you sell into, the materials you handle and the packing and documentation you need.